Warehouse Bottleneck: How to Find the One Step Holding Back Your Building

Every building has one step that sets the pace for everything else. That step is your warehouse bottleneck. On an average day it hides. At peak it shows up as overtime, late trucks, and a floor full of people who are busy but not winning.
This guide shows you how to find your bottleneck using data you already have, confirm it on the floor, and fix it in the right order. It takes three exports, a simple capacity check, and a walk.
What a warehouse bottleneck is
A bottleneck is the step whose capacity is lower than the demand placed on it. The building can only ship as fast as that step allows.
Work piles up in front of it. The steps after it sit idle and wait. Improving anything other than the bottleneck does not raise output, which is why so many improvement projects feel busy and change nothing.
A worked example (illustrative numbers)
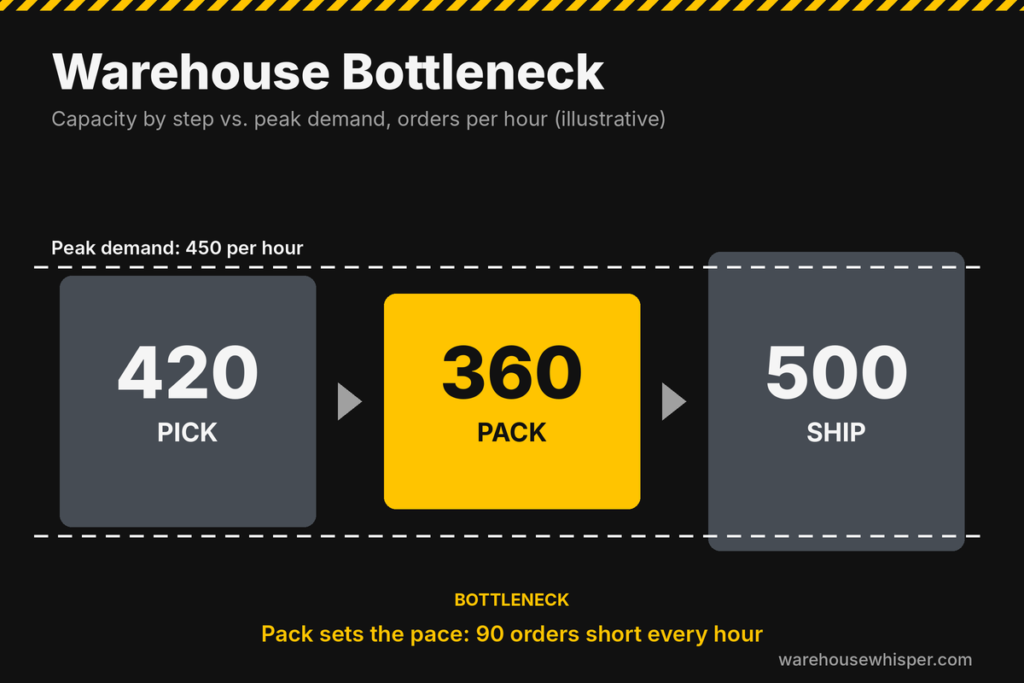
Take an e-commerce building with a 10-hour peak shift and a peak demand of 450 orders per hour.
| Step | Capacity (orders per hour) |
|---|---|
| Pick | 420 |
| Pack (12 stations at 30 per hour) | 360 |
| Ship | 500 |
Pack is the lowest at 360, so the building ships 360 an hour. That is 90 orders short every hour, or 900 orders carried over after the shift.
Now fix it the cheap way first. Ship has 50 orders an hour of spare capacity, so move people from ship to pack, release work to pack at the pace it can handle, and pre-stage packaging. If that is not enough, add three pack stations to reach 450.
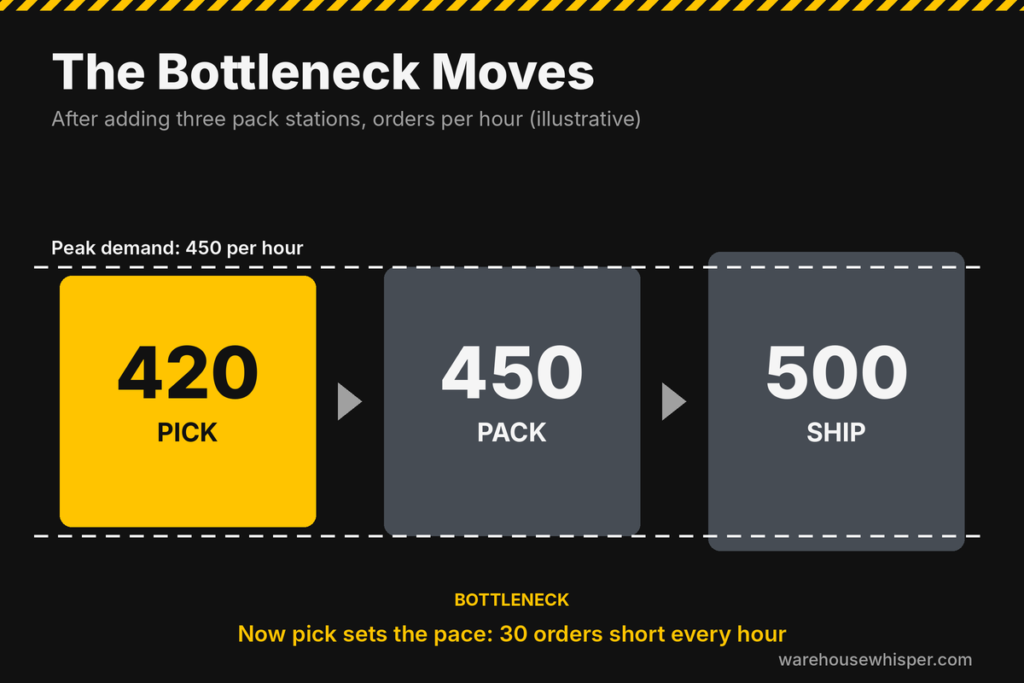
Then look again. Pick at 420 is the new constraint, and you are still 30 an hour short, or 300 orders over the shift. The bottleneck moved. That is normal, and it is why you check again after every fix.
How to find your warehouse bottleneck in 5 steps
1. Build the demand curve
Pull orders by hour for your busiest weeks. Use the peak hour, not the average. A bottleneck that does not show up in the daily average will show up in the peak hour.
2. Measure capacity by step
For each step (receiving, putaway, replenishment, pick, pack, ship), calculate capacity as the real rate per person times the people available. Use actual rates from your labor data, not the standard in the engineered labor model.
3. Compare capacity to demand
Put the capacities next to the peak demand. The step with the lowest capacity relative to demand is your suspect.
4. Walk the floor to confirm
The data tells you where to look. The floor tells you if it is true. Look for:
- Work queued in front of the suspect step
- Steps after it standing idle or starved
- Overtime concentrated at that step
- Workarounds people have built to cope
If you want a method for reading a building quickly, see how to read a building in four hours.
5. Find out what is causing it
A bottleneck is not always a machine. Check these before you spend money:
- Work release: are waves or batches released at the pace the step can handle, or dumped on it all at once?
- Replenishment timing: are pickers waiting on stock that was supposed to be there?
- Labor placement: are people where the constraint is, or where they were assigned last month?
- Cutoffs and carrier pickups: do they force a surge into one step?
- System response: is the WMS slowing a step down?
Many constraints turn out to be decisions, not equipment.
Where warehouse bottlenecks hide
- Receiving and putaway: trucks waiting, product staged on the dock, stock not available to pick
- Replenishment: pick faces empty at the worst moment
- Pick paths: congestion in the aisles with the fastest-moving items, often a slotting problem (see SKU slotting)
- Pack stations: the most common one in e-commerce
- Induction and sortation: the feed rate into automation
- Shipping: carrier cutoffs and dock door limits
- Labor imbalance: one shift or function carrying more than its share
Test your theory before you spend money
Here is a move most guides skip: try to blow up the bottleneck on purpose.
Pick the step you think is the constraint and temporarily put enough extra labor on it to push its capacity well past demand, for a shift or two. Then watch the whole building.
- If your theory is right, throughput rises everywhere. People who were standing idle downstream start working, and you often get the lift with the same total labor. That is easy savings.
- If throughput does not move, your suspect was wrong, and you learned that in a few hours instead of after a capital project.
If it works, you now have proof and a number. You can capture those savings and use them to justify a permanent fix, including new technology at that step. The test may cost some extra labor for a short time. It is worth it.
How to fix a warehouse bottleneck
The Theory of Constraints, introduced by Eliyahu Goldratt in his 1984 book The Goal, gives a simple order of operations, called the five focusing steps. The Lean Enterprise Institute explains how it fits with lean thinking. In warehouse terms:
- Identify the constraint, using the five steps above.
- Exploit it. Get every minute out of the step you already have. Keep it fed, cover breaks and shift changes, and take non-essential tasks off it. If receiving is the constraint, staff it fully and schedule inbound shipments so it never sits idle.
- Subordinate everything else to it. Release work and place labor to match the constraint, not to make every step look busy. If picking is the constraint, other areas adjust their schedules and workloads so picking is never starved or blocked.
- Elevate it. Only now add capacity: more stations, more people, or equipment.
- Repeat. Another step is now the limit. Go back to step 1.
Most buildings skip straight to step 4. That is how you end up buying equipment for a problem that a wave release change or a labor move would have solved.
What I see on the floor
Have you watched operators try to reduce the bottleneck by stacking completed customer orders on the floor between packing and shipping? Everyone wants to keep processing but no one realizes that the time it takes for you to downstack and then restack these boxes on the floor, you could have spent idle. Shipping cannot go any faster.
Peak makes it worse
Peak is when a bottleneck costs the most, because demand rises and the slack disappears. If you want to know where your building will break, look at the peak hour, not the average. For a wider view of getting ready, see 5 costly mistakes warehouses make during peak season, and track the right numbers with warehouse KPIs.
If you read one book
Read The Goal by Eliyahu Goldratt and Jeff Cox. It is a novel about a plant manager, Alex Rogo, trying to save a failing factory, and it teaches the Theory of Constraints through his story. It is about manufacturing, but every idea in this post applies to a DC. Here is a summary if you want a preview.
Want a second set of eyes on your building?
This is what the one-week operations review does. You send four standard exports, I walk the floor, and in five days you get a ranked list of where your building loses time and money, plus the first fixes. No equipment to sell.
Warehouse bottleneck FAQ
What is a bottleneck in a warehouse?
A warehouse bottleneck is the step whose capacity is lower than the demand placed on it. It limits how much the whole building can ship, and work queues up in front of it while later steps wait.
How do you identify a bottleneck in warehouse operations?
Pull orders by hour to find peak demand, calculate capacity for each step from real labor rates, and compare them. The step with the lowest capacity relative to demand is your suspect. Confirm it on the floor by looking for queues in front of it and idle steps behind it.
Is a warehouse bottleneck always a machine?
No. Many bottlenecks come from how work is released, when replenishment happens, where labor is placed, or how carrier cutoffs force a surge. Check these before buying equipment.
Why does the bottleneck move after I fix it?
Once the slowest step speeds up, the next slowest step becomes the limit. This is normal. Check capacity against demand again after every change.